


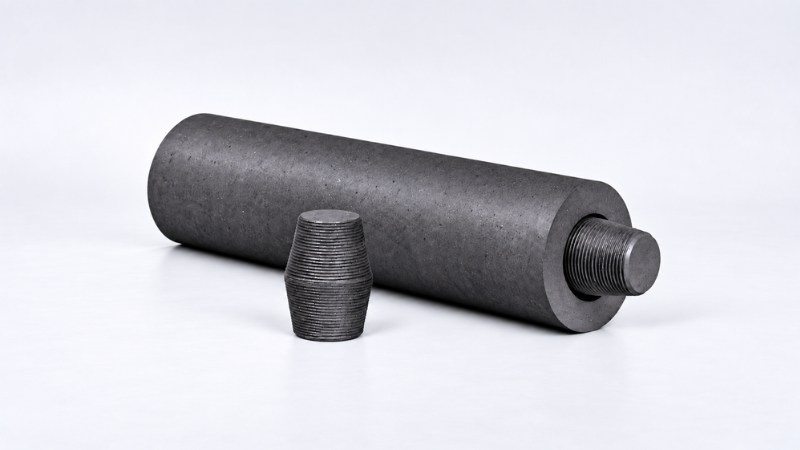
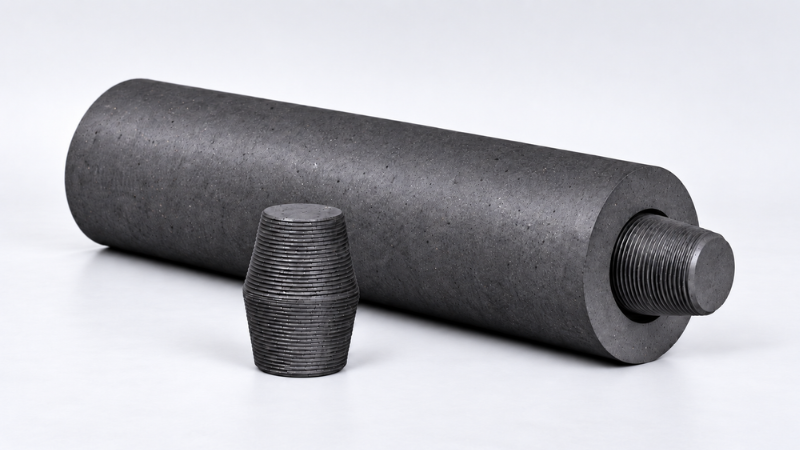
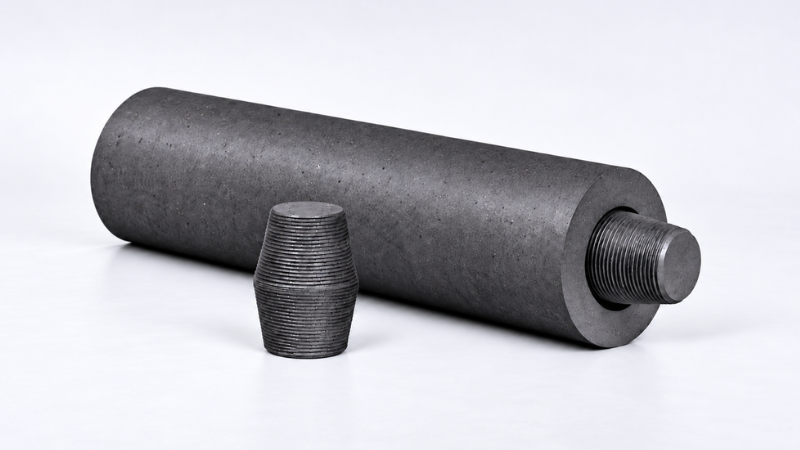
Graphite electrodes are high-temperature electrical conductors used primarily in electric arc furnaces (EAF) and ladle furnaces (LF). They carry electrical current into the furnace, where electric arcs provide the thermal energy required for steel melting and refining.
SATRAD supplies RP, HP and UHP graphite electrodes with compatible connecting nipples.
| Grade | Available diameters (mm) |
|---|---|
| UHP | 400, 450, 500, 550, 600, 650, 700, 750, 800 |
| HP | 200, 250, 300, 350, 400, 450 |
| RP | 150, 200, 250, 300, 350, 400, 450, 500, 550, 600 |
Chemical composition (% by mass)
| Grade | Fixed Carbon ≥ | Ash ≤ | Volatile Matter ≤ | Moisture ≤ | Sulfur ≤ | Nitrogen ≤ |
| Special Grade | 99.7 | 0.15 | 0.15 | 0.2 | 0.01 | 0.002 |
| Grade 1 | 99.5 | 0.20 | 0.30 | 0.3 | 0.02 | 0.015 |
| Grade 2 | 99.0 | 0.50 | 0.50 | 0.5 | 0.03 | 0.020 |
| Grade 3 | 98.5 | 1.00 | 0.50 | 0.5 | 0.05 | 0.030 |
Note: All values are mass fractions. Except for moisture, all values are expressed on a dry basis.
Graphite electrodes are produced through five main stages, from raw material preparation to final machining.
Selected coke materials are crushed, screened and graded to the required particle sizes.
Prepared coke materials are mixed and kneaded with coal tar pitch binder to form a homogeneous paste, which is then shaped into green electrodes, typically by extrusion.
The green electrodes are baked to carbonize the binder and develop the required mechanical strength. Depending on the grade and manufacturing process, pitch impregnation and rebaking may be performed to increase density and improve material properties.
The baked electrodes undergo high-temperature treatment to develop a graphite structure, improving electrical and thermal conductivity and establishing the required material properties.
Electrode bodies and nipples are machined to specified dimensions and connection tolerances, including the threaded sockets and nipples required for secure electrode assembly.
For a detailed explanation of each stage, read Graphite Electrode Manufacturing Process: Step-by-Step Guide.
Graphite nipples connect electrode sections into a continuous column, carrying electrical current while withstanding mechanical and thermal loads during furnace operation. SATRAD supplies matching nipples according to electrode diameter, thread design and connection dimensions. See Graphite Electrode Nipples for 3TPI and 4TPI dimensions, compatibility and handling information.
Graphite electrodes conduct high electrical currents to generate electric arcs for melting steel scrap, direct reduced iron (DRI), and other metallic charge materials.
Ladle furnaces use graphite electrodes to provide arc heating during secondary steel refining and temperature adjustment.
Three graphite electrodes typically operate with three-phase alternating current to generate electric arcs for melting and refining.
DC electric arc furnaces typically use a single graphite electrode column, assembled from electrode sections connected by threaded nipples. The electrode system is designed to accommodate high operating currents and demanding thermal conditions.
The grades differ in their electrical, mechanical, and thermal properties and their suitability for different furnace operating conditions. UHP electrodes are generally designed for higher current-density applications, while HP and RP grades serve less demanding electrical operating ranges.
Electrical resistivity affects resistive heating and electrical losses in the electrode column. Lower resistivity can be beneficial under high electrical loads, but electrode selection must also account for mechanical properties, thermal behavior, and connection performance.
Yes. Matching nipples can be supplied according to the specified electrode diameter, thread design, and dimensional requirements.
Consumption depends on electrode material, current loading, furnace temperature, oxygen exposure and operating practices. Breakage, spalling and connection failures can add to material losses; comparisons in kg/t-LS should use a consistent calculation basis. Read Graphite Electrode Consumption in EAF for the operating factors and performance review.
Common contributing factors include mechanical impact, excessive bending loads, damaged or improperly assembled connections, thermal stresses, and unsuitable operating conditions. A reliable diagnosis requires examination of both the failed electrode and the furnace operating history.
Typical checks include electrical resistivity, bulk density, flexural strength, electrode dimensions, surface condition, and socket and nipple thread accuracy. Test methods and acceptance criteria should follow the agreed product specification. See Graphite Electrode Quality Inspection and Testing for the detailed inspection items.
Protect electrodes from impact, excessive loading, moisture-related contamination and damage to machined connection surfaces. Use suitable supports and handling equipment, and inspect and clean the nipple, socket and mating surfaces before assembly. Read Graphite Electrode Packaging, Storage and Handling for the transport, storage and pre-assembly guidance.
Please provide the electrode grade, diameter, length, nipple specification, required quantity, delivery destination, and any additional technical or inspection requirements. You can send your inquiry directly to our sales team at info@satradco.com for a quotation and technical assistance.
SATRAD supplies RP, HP, and UHP graphite electrodes for electric steelmaking applications.
Please provide the electrode grade, diameter, length, nipple specification, required quantity, delivery destination, and any additional technical or inspection requirements. You can send your inquiry directly to our sales team at info@satradco.com for a quotation and technical assistance.

Scan the QR code to chat with us